This guide explains what Colbate is, where it fits in material selection, and how to evaluate suppliers based on testing, purity, and handling requirements. Objectively, it discusses how colbate-related products are specified in industrial and technical contexts, what documentation to request, and what conditions typically affect performance and reliability across projects.
If you’re considering Colbate for an industrial or technical application, the very important starting point is not marketing claims—it’s verifiable specification: the exact grade, purity/chemistry, particle or surface characteristics (when relevant), allowable contaminants, and traceable documentation. A credible supplier can also explain storage, compatibility, and quality-control checkpoints that reduce variability from batch to batch.
In practice, buyers evaluate Colbate through a disciplined process: define performance requirements, request test reports aligned to recognized methods, confirm packaging and traceability, and validate handling conditions. This approach is especially valuable when the material influences downstream performance, safety, or yield.
It’s also worth recognizing that the term “Colbate” can function like a label in certain supply chains—sometimes referencing a family of related materials, sometimes a specific commercial grade, and sometimes a trade shorthand that differs by region. That is why “specification-first” due diligence is not optional. When your project depends on consistency, the only reliable way to reduce uncertainty is to demand documents that tie directly to the batch you will receive.
Finally, understand the role of Colbate in your overall process. A material might not be difficult to obtain, but if its properties influence critical parameters—such as reaction kinetics, compatibility with binders, electrical characteristics, corrosivity, moisture sensitivity, or contamination sensitivity—then “good enough” becomes a risk. In those cases, a supplier’s ability to provide repeatable results and to help troubleshoot deviations often matters as much as the initial paperwork.
In technical procurement, “Colbate” may be referenced as a material name used within specific supply chains or formulations. Because terminology can vary by region, industry, or manufacturer, objective due diligence is essential. Rather than assuming a universal meaning, professionals treat Colbate as an item that must be mapped to an exact specification before purchase.
Across many materials markets, buyers ultimately care about the same fundamentals: the chemistry (or relevant composition), consistency of physical properties, and the supplier’s ability to document results using standardized testing. When these elements are aligned, buyers can manage performance risk and integrate the material into established processes more predictably.
Procurement teams often encounter Colbate in scenarios such as the following (illustrative examples of typical procurement patterns, not assumptions about a single industry):
Because of this variety, the procurement process should focus on linking Colbate to a concrete grade definition and confirming that the grade is stable across time and manufacturing location. “Same name” across suppliers is not the same as “same specification.” Even small differences—like a slightly different impurity limit, particle size distribution range, or residual solvent profile—can be the difference between meeting a production specification and failing quality checks.
An expert procurement lens typically focuses on five areas. If you handle only one step, make it the specification confirmation stage—because it prevents costly mismatches later.
To expand each area into practical procurement actions, consider these deeper checks:
One useful procurement mindset is to treat Colbate as a “chain of custody” item for critical properties. If the material’s performance is influenced by chemical purity, trace contaminants, or physical attributes, then any step between manufacturing and use can matter: container selection, transit conditions, receiving storage, and even the time you hold inventory before consumption. Your evaluation should consider the entire chain, not just the CoA.
Buyers often ask for Colbate price information, but prices can vary widely based on grade, test scope, packaging, minimum order quantity, shipping terms, and lead time. In responsible procurement, “price” is top treated as part of a total commercial picture rather than a single number.
To make price comparisons meaningful, request itemized quotes that separate:
If a supplier offers a “one-size-fits-all” price without linking it to a defined specification, that is a warning sign for technical projects. A professional quote should connect commercial terms to technical deliverables. In other words, the quote should answer: “What exactly are you paying for?”
There are also practical reasons not to rely on a single market number. For example:
When comparing offers, it helps to convert each quote into a comparable “total landed cost” and include risk-based considerations. For critical processes, consider a “cost of uncertainty” approach: if limited documentation increases the chance of a quality escape or a production hold, the cheapest quote can become expensive. This is why procurement should coordinate with quality and production teams when evaluating Colbate purchases.
When assessing Colbate supplier details, the goal is to verify both capability and accountability. Industry buyers usually ask for documents that prove the supplier can consistently meet the described requirements.
Request the following where applicable (and ensure they correspond to the exact grade you plan to purchase):
Also confirm whether the supplier provides pre-shipment inspection or additional verification on request. If your use case is sensitive to contamination or variability, these added checkpoints can reduce risk.
Beyond the baseline list, you can also ask a supplier some high-value questions that often reveal maturity:
When suppliers respond clearly—with consistent documentation, method references, and traceable IDs—you usually see lower project friction later. When suppliers respond vaguely—e.g., “we meet the requirements” without showing the data—buyers should treat that as a risk to be mitigated before purchase, not after delivery.
Because Colbate may appear in distinct supply chains, it can be encountered in multiple technical contexts. The common thread is that it is selected when its documented characteristics align with a downstream requirement—such as performance stability, compatibility with processing steps, or controlled material behavior.
In an objective selection framework, you should align Colbate to three practical questions:
To make these questions operational, define what your “functional requirement” means in measurable terms. Examples of measurable requirements include:
Compatibility also needs definition. Compatibility isn’t just about chemical reactions; it also includes process handling realities such as:
Finally, validation within constraints means understanding your ability to test quickly and to stop production if something is wrong. If your process cannot tolerate delays, you may need stronger supplier pre-verification. If you can test incoming material and hold product before release, you can manage risk with incoming inspection plus retention sampling.
From an industry expert standpoint, the highest-impact risk reductions are usually procedural rather than purely technical. Even when a supplier meets baseline specifications, performance can degrade due to handling, timing, or integration errors.
Therefore, professionals often recommend:
This is particularly important when the material’s effect is amplified further downstream—where small deviations can become large outcomes in yield, quality consistency, or reliability.
To expand the “procedural over purely technical” idea, consider the typical failure modes procurement and quality teams see in practice:
Risk reduction therefore becomes a coordinated set of controls across departments. Procurement ensures correct specification and documentation; quality ensures batch-linked inspection and test methods; operations ensures handling and process integration; and EHS ensures safe storage and compliance. When these controls operate together, Colbate procurement becomes repeatable rather than reactive.
The following table compares the typical “supplier offer” components you should verify when sourcing Colbate. Treat it as a checklist to standardize evaluation across vendors.
| Evaluation element | What to look for | Why it matters for Colbate |
|---|---|---|
| Grade and composition | Exact grade name and documented composition ranges | Prevents specification mismatch and process failures |
| Batch traceability | Lot/batch identifiers tied to the CoA | Enables root-cause analysis if performance deviates |
| Testing evidence | CoA with test methods and results | Confirms that claims match measurable outcomes |
| Contaminant limits | Clear allowable impurities and detection/measurement scope | Reduces compatibility and downstream defect risk |
| Packaging and shelf conditions | Pack type and supplier-stated storage guidance | Protects against variability caused by handling exposure |
| Lead time and availability | Defined dispatch timelines for the specified grade | Supports production planning and reduces downtime |
| Commercial transparency | Itemized pricing tied to deliverables | Enables accurate comparisons across quotes |
| Corrective actions | Process for nonconformances and documented remediation | Improves continuity if issues arise |
When you use this table in a real sourcing process, the most useful output is not just a “pass/fail” score. It’s also a list of gaps—specific missing documents, unspecified tolerances, or unclear traceability practices. Those gaps become your procurement action items (and often your negotiation points) before the purchase order is issued.
Below is a step-by-step procurement approach that many operations teams use to control variability. Adjust the depth of each step depending on criticality, but keep the logic intact.
To strengthen this guide, many teams add two controls at points where issues typically occur:
To reduce integration risk, establish the following conditions up front. These requirements are framed generally because the exact operational constraints depend on your process and the Colbate grade.
In more detail, a robust checklist often also includes:
“Colbate” is commonly used as a material name in technical procurement, but the precise definition can vary by grade or supply chain context. The very objective answer is the one tied to an exact grade specification and documented composition/performance characteristics from the supplier.
In many procurement environments, what matters is not the brand-like name but the underlying specification parameters. The same “Colbate” label might map to different compositions or different impurity profiles unless you confirm the grade sheet. If your internal engineers or QA teams rely on a specific parameter set, you should ensure that the supplier’s grade corresponds to those same parameter sets.
Request the grade name and a specification sheet that includes composition ranges, impurity limits, and any measured performance criteria. Then require a batch-linked Certificate of Analysis for the lot you will receive.
To make this confirmation robust, also check that the grade sheet is current. Some suppliers supersede grades over time, so a specification sheet referenced in an old quote may be outdated. Ask the supplier to confirm whether the grade has changed and whether the quote reflects the latest spec. If your internal system includes approved vendor/approved grade catalogs, ensure the requested grade is cross-referenced properly.
Typically: a Certificate of Analysis tied to the batch/lot, handling documentation (such as a safety document), test methods or measurement scopes, and traceability identifiers. For higher criticality applications, you may also request additional verification or pre-shipment inspection.
Documentation quality matters as much as documentation presence. A complete CoA should include traceability identifiers, results, method references (or at least method descriptions), and the date of testing if available. A “summary CoA” that does not specify what was measured or how can be insufficient for critical uses. If you require internal verification, ask whether the supplier’s analytical methods are compatible with your internal test capabilities or whether your QA team must retest.
Compare quotes only after verifying that the technical specifications match. Look for itemized pricing tied to deliverables (including test certificates, packaging, lead time, and logistics) rather than relying on a single unit price comparison.
When comparing, check whether different quotes include the same scope of documentation. If one supplier’s price includes a full CoA with specific test methods and another’s includes only partial tests, the “cheaper” quote may not be comparable. Another common mismatch involves packaging: the supplier might price one quote for a protective package and another quote for a standard package that increases contamination risk. Your price comparison should include the packaging and handling implications relevant to your process.
Standards differ by industry and grade. The objective method is to ask your supplier which test methods they use for the relevant properties and whether those methods align with recognized practices in your field. Your internal QA team can then confirm suitability.
In practice, suppliers may use a variety of analytical techniques depending on the material properties you care about. For instance, properties such as composition, impurity levels, moisture, particle size distribution, or residue content might require different testing approaches. The key is alignment: the test method should measure the property in a way that supports your risk assessment and your release criteria.
Common risks include documentation mismatch, packaging damage, incorrect storage conditions, and unrecorded lot identifiers. Establish receiving controls and storage compliance to reduce variability and support traceability if issues arise.
Receiving and storage risks are often “avoidable” once they are identified. For example, you can minimize documentation mismatch by requiring that the lot number on the CoA matches the lot number on the packaging label. You can minimize packaging damage by inspecting container seals and verifying that protective coverings are intact. You can minimize storage drift by using clear labeling, defined environmental conditions, and controlled access to the storage area. Unrecorded lot identifiers are minimized by using a standardized receiving workflow and barcoding or similar traceability tools where feasible.
If the material is new to your process, a pilot is often prudent—especially for applications where tight tolerances affect yield, quality, or safety. For mature, well-characterized workflows, some teams may reduce scope, but they still validate critical parameters at least once per new grade or supplier.
A pilot test should be designed for decision-making rather than general observation. Define acceptance criteria up front (e.g., yields, defect rates, stability over time, and any relevant performance metrics). Include comparison against a baseline material or previous supply performance if possible. Also plan the pilot sampling strategy so that you can diagnose whether any deviations are due to Colbate itself or due to integration differences.
Select suppliers based on specification alignment, documented evidence (CoA/test methods), traceability maturity, and handling guidance. A supplier’s ability to support audits and corrective actions is a strong indicator of process reliability.
To further sharpen supplier selection, you can compare not only “what they say” but “what they do when something goes wrong.” Ask for examples of how nonconformances were handled historically (within confidentiality boundaries). You can also evaluate whether the supplier provides consistent documentation formats and whether their traceability information is easy to integrate into your systems. The suppliers that reduce friction in documentation and lot tracking typically reduce operational workload and quality risk.
Qualification typically includes: specification review, document validation, receiving/storage capability checks, pilot performance confirmation (when required), and a documented corrective-action/feedback loop for nonconformances.
Many qualification processes also include a “repeatability” component. For example, you might require successful performance across multiple consecutive lots, not just a single pilot lot. Repeatability reduces the chance that the first lot was an exceptional case. Additionally, you can test the supplier’s responsiveness: how quickly do they provide documentation corrections, how they handle a lot hold request, and whether they help diagnose the root cause when performance deviates.
For technical integrity, you should avoid committing based solely on high-level claims. Batch-linked documentation is important because performance characteristics can vary between lots even within the same grade.
At minimum, require enough information to confirm that the supplier can deliver the specified batch quality, not only that they can produce it in principle. If a supplier cannot provide batch-linked CoA at time of delivery planning, you may negotiate conditions such as: material receipt on hold until CoA verification, additional internal testing at receipt, or a replacement/credit policy if documentation or performance does not match the agreed specification.
If you operate in a multi-site environment, align internal language for “Colbate” and grade naming. Procurement teams often find that supplier catalogs use shorthand terms that correspond to different sub-grades. A short internal alignment workshop—naming, specs, receiving checks, and documentation requirements—can prevent the kind of confusion that delays projects.
Localization can also affect regulatory and compliance requirements for safety documentation. Even when the material identity is the same, the required labeling format, the safety document template, and the language expectations may differ by region. Your qualification process should include confirmation that the supplier can supply compliant documents for your sites, including local versions of relevant safety documentation, if required.
When evaluating materials procurement, anchor your internal requirements to widely used quality and risk frameworks. For example, the ISO quality management family supports supplier qualification and traceability principles, while internationally recognized safety and chemical handling documentation practices help ensure safe use. For environmental and compliance expectations, consult applicable local regulations and your organization’s EHS policies.
Sources for reference (general guidance): ISO 9001 (quality management systems); ISO 22000 (food safety management systems where relevant); and globally adopted chemical safety documentation practices such as the GHS framework as implemented through local regulatory regimes.
It’s important to treat these frameworks as structural guidance, not as a substitute for the material-specific specification. For example, ISO 9001 certification suggests the supplier has a quality management system, but it does not automatically guarantee that a specific grade of Colbate meets your purity or impurity thresholds. The supplier’s documented processes must translate into the correct outputs for your specific order—evidenced by batch-linked documentation and measurable test results.
Similarly, GHS-aligned safety documentation helps ensure correct handling and risk communication, but safety documents alone do not confirm that the material meets the functional performance requirements of your process. Procurement should therefore require both: safety compliance documentation and technical specification documentation.
Colbate sourcing succeeds when specification alignment comes before price, and documentation comes before delivery acceptance. By evaluating grade clarity, batch traceability, testing evidence, and supplier handling guidance—and by applying a step-by-step qualification process—you can reduce technical risk while improving consistency across projects. Whether you are comparing supplier details, reviewing Colbate price information, or planning storage and receiving workflows, the objective priority remains the same: match measurable specifications to your measurable needs.
To operationalize this conclusion, ensure your organization can consistently perform the “specification-first” discipline: require the correct grade definitions in writing, demand batch-linked documentation, and define internal receiving and release criteria. When those controls are in place, your team can use supplier offers confidently and can respond quickly if performance varies. That is what transforms Colbate procurement from a transactional purchase into a controlled technical supply process.



This guide explains what Xiva is, how suppliers structure pricing, and what to verify before purchasing. Objectively, Xiva is treated as a product or brand identifier used in sourcing and retail listings. Background sections cover procurement considerations, quality checks, and documentation standards, helping buyers compare offers without relying on marketing claims.
This guide explains how 1993-based context can help interpret supply chains, procurement decisions, and supplier reliability in today’s markets. Objectively, “1993” often functions as a reference point in sourcing histories, documentation practices, and product lineage, while supplier-related terms indicate where accountability, traceability, and quality controls are documented across time.
This guide explains how to interpret 1993-era decisions, sourcing choices, and supplier relationships using a disciplined research approach. It then provides objective background on common meanings of “1993” in records, the role of suppliers in quality assurance, and why later due diligence matters for procurement and compliance decisions. No claims are exaggerated; methods emphasize verifiable documentation.
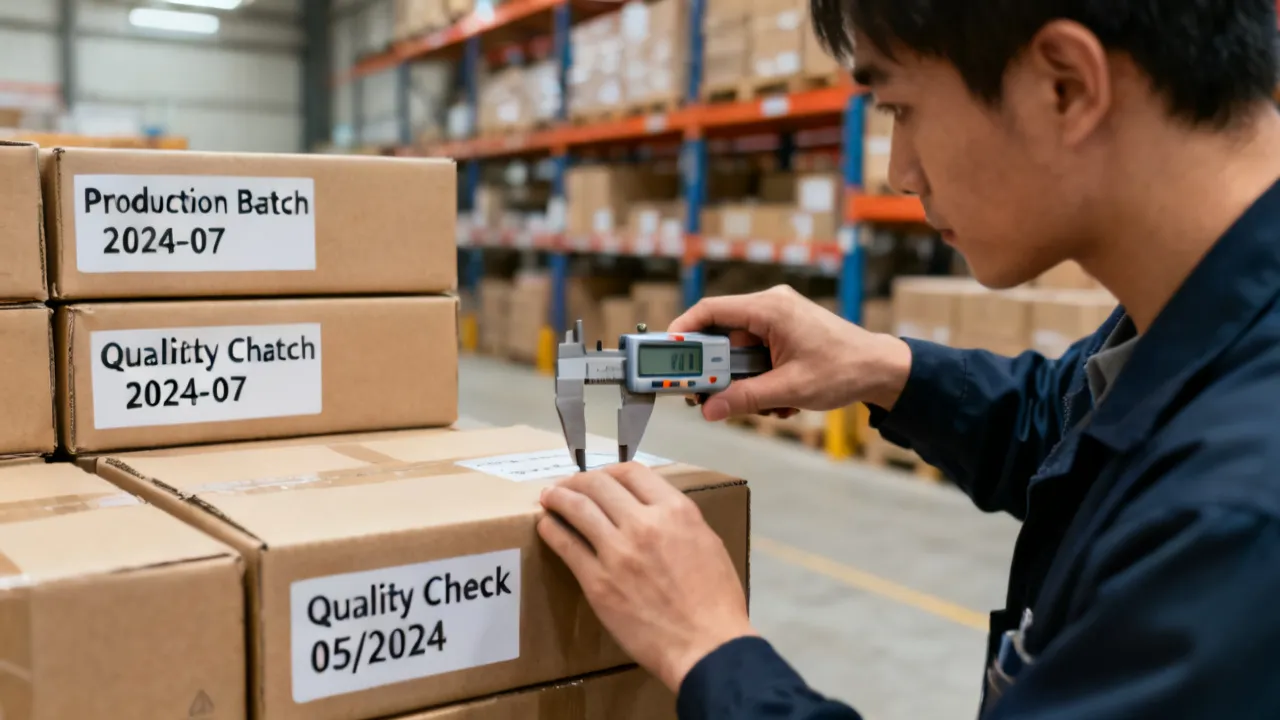
This guide explains how batch or lot identifiers like 16121978 support traceability, quality control, and compliant documentation across suppliers. Objectively, these identifiers connect products to manufacturing records, testing outcomes, and distribution history. We also compare practical requirements for accurate recordkeeping, highlight common risks, and provide expert-led FAQs for procurement and quality teams.
This guide explains how 1993-era product value, supply chain choices, and good vendor relationships shape modern purchasing decisions. It provides objective background on the roles of suppliers, pricing discipline, and documentation practices. It also outlines evaluation conditions readers can apply to assess sourcing risk and maintain quality across time.
This guide explains how the year 1993 continues to influence today’s market expectations and supplier practices. Objectively, 1993 sits in a period of expanding global trade, evolving quality norms, and digitization experiments that shaped procurement thinking. The article connects these themes to practical decision-making, evaluation criteria, and service purchasing habits, helping readers interpret “legacy” without assuming myths.

