This guide explains Fulepelata in an objective, practical way—covering what it typically is, how quality is assessed, and how sourcing decisions affect performance. Background context is provided for readers comparing suppliers, lead times, and material consistency, without relying on claims that can’t be verified.
When considering Fulepelata, the most consequential decision is not just availability—it’s verifiable quality controls: consistent material specifications, traceable sourcing, stable packaging, and transparent supplier terms. Treat Fulepelata as a product category where small differences in inputs can noticeably affect final appearance and durability, so your evaluation should start with documentation and end with a controlled test lot rather than assumptions.
In practice, “quality” for finish-dependent categories rarely means a single attribute. It’s usually the combined behavior of raw inputs, processing steps (coating, finishing, curing, treatment, or surface modification), handling during transport and storage, and the effectiveness of the supplier’s inspection discipline. If you don’t control and verify those inputs, even a supplier that has delivered good results in the past can unintentionally ship a different internal configuration—one that still “fits the name” but not the performance you expect.
Therefore, the key takeaway is to treat Fulepelata sourcing like a process problem, not a product name problem. You reduce risk by requiring evidence: specification sheets, lot traceability, inspection reports or inspection methods, clearly written order terms, and handling/storage guidance that is specific enough to prevent outcomes from drifting. Then, you validate using a controlled test lot evaluated under your actual handling and process environment.
The term Fulepelata is commonly used in commerce to describe a category of finished goods associated with specific material treatments and surface characteristics. In real-world procurement conversations, buyers usually look for three things: (1) a consistent finish, (2) dependable dimensional or performance behavior under normal use, and (3) predictable appearance over time.
Because product categories evolve by region and supplier, the most reliable approach is to evaluate Fulepelata based on the attributes stated in specifications—rather than relying on the name alone. If a supplier describes Fulepelata using measurable criteria (e.g., thickness, coating uniformity, finish type, handling characteristics), it becomes easier to compare offers across vendors.
It’s useful to think about how terms like “Fulepelata” function in procurement. They often act as a shorthand that bundles multiple internal process decisions into a single label. If two suppliers apply the label differently, you can get different outcomes even when both vendors insist their product is “Fulepelata.” That’s why procurement best practice is to map the label to a measurable attribute set. If the measurable attributes don’t exist or can’t be provided, your evaluation process should become more conservative (more extensive tests, stricter acceptance criteria, and shorter initial run sizes).
Depending on your industry, Fulepelata may be used in contexts where surface character is crucial (e.g., finishing-adjacent manufacturing, packaging skins, decorative or semi-decorative surface treatments, or applications where appearance and tactile feel affect customer perception). In those cases, subtle input changes (formulation changes, curing profiles, surface energy differences, or minor variations in base material) can affect both the look and the durability.
Price for Fulepelata should be treated as an initial signal, not a final proof of value. In many supply chains, the “best deal” can be the result of differences in inputs—such as varied source materials, less rigorous finishing, or shorter aging/curing processes. Conversely, a higher price can reflect better documentation, tighter tolerances, and repeatable outcomes.
To assess whether an advertised price is meaningful, ask for the same baseline information from each supplier: material standard or grade, finishing method, quality inspection procedure, and typical tolerances. When those points are comparable, you can make an apples-to-apples decision grounded in total cost considerations (including handling, waste rate, and rework risk).
Total cost of ownership for Fulepelata frequently includes more than the purchase price. You should think about hidden cost drivers such as:
In other words, a cheap Fulepelata lot can be expensive if it creates uncertainty that forces you to either accept variability you don’t want or spend resources on requalification and reruns.
From an industry perspective, the supplier’s advantage is rarely a single factor; it’s the combined effect of process control and accountability. For Fulepelata, robust suppliers tend to provide:
Even if two offers list similar “Fulepelata” naming, the supplier’s process control can cause meaningful differences in the end product’s uniformity.
The “chain of custody” framing is valuable because it matches how problems occur in the real world. A lot’s final appearance might drift due to:
A supplier that can explain how they control these steps—and can document at least the key controlling points—reduces the chance that you’re buying “surprises.” Supplier selection should therefore be evaluated across the entire chain, not merely at the moment of shipment.
Instead of trying to judge quality by appearance alone, use a structured evaluation that mirrors how production teams assess inputs. An expert approach typically includes:
This methodology reduces the risk of accepting a cosmetically pleasing but inconsistent lot.
To make evaluation more efficient, you can design your checks around what tends to go wrong. For example, many finish-dependent categories show problems such as streaking, uneven gloss distribution, orange-peel-like texture, edge fraying, or adhesion inconsistency. Even when you can’t identify the root cause immediately, your evaluation can still detect the symptom and prevent downstream failures.
Efficiency also improves when you standardize your internal inspection rules. If one team member “accepts” a lot visually and another rejects it, you lose the ability to measure supplier performance over time. A better approach is to define internal acceptance criteria for at least:
Standardization turns evaluation into a repeatable procedure rather than a debate. Over time, that repeatability helps you negotiate better supplier terms and reduces the administrative burden of requalification.
Fulepelata is often chosen for applications where finish character and stability matter. In procurement terms, the “right” selection depends on how the product will be handled—temperature exposure, friction, moisture conditions, and downstream finishing steps can all influence the outcome.
If you’re integrating Fulepelata into a production process, request guidance on recommended handling and finishing compatibility. A supplier who can explain how their Fulepelata behaves in real workflows is usually investing in measurable process reliability.
A frequent mistake in sourcing finish-dependent categories is to assume the “same name” means the “same behavior.” Consider how a lot can behave differently depending on your environment. Even if the finish looks identical on arrival, your process might expose it to conditions that reveal differences, such as:
Therefore, when you request a “Fulepelata” variant, you should also request the supplier’s intended use profile. If the supplier can only provide generic statements, your organization should treat the product as higher risk and require additional testing under your real operating conditions.
The following comparison table highlights common conditions/requirements buyers should confirm when evaluating Fulepelata. It is framed for objective comparison—so you can align vendors to the same evaluation baseline.
| Evaluation Item | What to Request | Why It Matters for Fulepelata | Pass/Fail Indicators |
|---|---|---|---|
| Product Specification | Material grade/standard, finish type, thickness or relevant measurable attributes, and documented tolerances | Ensures “Fulepelata” refers to the same quality profile across suppliers | Specification matches your use-case requirements; tolerances are clearly stated |
| Lot Traceability | Batch/lot numbering method and documentation package for each shipment | Allows you to isolate variations and reduce downstream rework risk | Lot ID is present and documented; batch history can be shared |
| Quality Inspection | Inspection frequency, measured parameters, and acceptance criteria | Process control predicts consistency more than marketing claims | Inspection metrics are stated; acceptance thresholds are defined |
| Packaging & Storage Guidance | Storage conditions, shelf-life expectations, and handling instructions | Surface outcomes can shift due to improper storage even when inputs are correct | Guidance is specific; packaging supports the recommended conditions |
| Lead Time and Order Terms | Typical lead time range, delivery schedule rules, and order quantity conditions | Operational planning depends on realistic production timing | Lead times are coherent; terms are clearly written |
| Test Lot Policy | Availability of sample sizes, test-lot procedure, and replacement/claim process | Validates compatibility with your process and acceptance criteria | Clear test method; documented claim process for nonconforming lots |
To deepen the practical utility of this comparison table, consider adding internal scoring categories. For each evaluation item, assign a score such as “documented and clear,” “documented but incomplete,” or “not provided.” That gives you a structured way to compare suppliers even if they present information in different formats. In procurement negotiations, you can use that scoring as evidence of due diligence.
Also remember that you’re not only comparing suppliers—you’re comparing uncertainty. A supplier that provides full documentation and a robust test/claim policy reduces operational uncertainty, which often has direct financial impact even if the unit price looks slightly higher.
Below is a practical, step-by-step guide aligned with procurement best practices. It’s designed to help you compare suppliers consistently and reduce variability risk.
Start by writing down what Fulepelata must deliver in your context: appearance uniformity, tactile characteristics, dimensional stability (if relevant), and compatibility with downstream processing. If you don’t define these requirements first, supplier comparisons can become superficial.
When defining “must-have” attributes, do not only include what you can see. Include what your process does to the product. For example, if your process involves pressing, cutting, heat exposure, bonding, or repeated handling, you should translate that into attribute requirements: resistance to deformation, stability under thermal cycling, adequate adhesion behavior, and defect tolerance boundaries.
It can also help to define:
Even if you cannot measure every characteristic with instruments immediately, you can still define categories and response actions. This becomes especially valuable during the initial test lot.
Ask for a specification sheet, tolerance or acceptance criteria, and the quality inspection approach. If a supplier can’t provide any technical documentation for Fulepelata, treat that as a red flag—not necessarily a deal-breaker, but a reason to test more thoroughly.
Good documentation reduces both technical and contractual ambiguity. In your documentation request, aim to get answers to these questions:
Additionally, ask for the supplier’s typical deviation or nonconformance process. A mature supplier will explain what happens if a lot does not meet internal standards. This “what happens when things go wrong” insight often correlates strongly with actual quality outcomes.
When evaluating price for Fulepelata, consider the full offer: packaging, storage instructions, lead time, minimum order quantity, and claim handling. The lowest advertised price can still be expensive if it increases waste rate or requires rework.
To apply this step rigorously, translate offer terms into operational impacts. For example:
This is where procurement and quality teams should collaborate. Quality teams can estimate potential risk impact; procurement can estimate contract risk and costs. Together, you can compare suppliers fairly.
Request a test lot and evaluate it under your actual handling conditions. This step often reveals issues that are invisible in static samples—especially if the product experiences friction, moisture, heat, or repeated finishing steps.
A “controlled test lot” should be treated as a mini-production run under your real workflow. That means controlling variables and documenting everything. Even if you don’t have laboratory-grade instruments, you can still design a test process that yields actionable results.
For example, you can design your test as follows:
Then decide acceptance criteria before the test begins. If you define criteria afterwards, you can bias the evaluation. Pre-defined criteria also support supplier claims if you discover nonconformance.
During testing, assess how quickly the supplier responds with clarifications and whether they can support the documentation you requested. In mature supply relationships, responsiveness is a reliable indicator of process discipline.
Supplier responsiveness can be measured informally but consistently. Consider tracking:
While responsiveness isn’t a direct substitute for quality, it reduces your risk during troubleshooting. A supplier who can quickly explain how their process works is often a supplier who controls it.
Do not rely only on “it looks good.” Approve the lot that meets your predefined acceptance criteria for Fulepelata, and record the results so future comparisons are easier and faster.
When you finalize selection, document the lot(s) you accepted and what you measured or observed. This record supports several benefits:
It can also be helpful to set a phased approval approach. For instance, you might approve the supplier conditionally for a limited volume first, then scale once multiple consecutive lots meet acceptance criteria.
In many manufacturing and finishing-adjacent categories, consistency is not guaranteed by the product name; it is guaranteed by the combination of supplier process control, input material uniformity, and inspection discipline. Buyers usually use structured evaluation to ensure that a product category like Fulepelata behaves predictably across shipments.
Where possible, align your evaluation approach with recognized quality management frameworks. For general reference, ISO 9001 is widely used as a baseline for quality management systems, emphasizing documented processes and continuous improvement (see ISO’s official materials for background). While ISO 9001 does not validate a specific product claim on its own, it can signal whether a supplier operates with quality discipline that supports consistency.
In more practical terms, many buyers implement a quality framework that includes:
For finish-dependent categories, this framework becomes even more important because appearance-based outcomes can shift subtly, and those shifts can correlate with process changes that aren’t visible without traceability and controlled evaluation.
Another industry reality is that buyers often face “spec drift,” where the supplier’s internal process changes over time due to formulation updates, equipment upgrades, or sourcing changes. A supplier might still produce something that is “close enough” by informal standards, but your application might be sensitive to the differences. That’s why lot traceability and revalidation triggers matter: you need a way to detect and respond when the product’s internal configuration changes.
Fulepelata is typically used in supplier and buyer discussions to refer to a finished product category characterized by specific material treatment and surface/handling attributes. Because definitions can vary by vendor, you should rely on the specification sheet and measurable attributes rather than the name alone.
Compare total offer terms: documentation quality, packaging and storage guidance, lead time reliability, lot traceability, and inspection criteria. If specifications differ, pricing is not directly comparable—even when the product name is the same.
Request the product specification, batch/lot traceability method, inspection parameters with acceptance thresholds, and handling/storage requirements. If available, ask for test-lot policy and a documented claim process for nonconforming goods.
No. Appearance can be a useful starting point, but consistent finish over time and under real handling conditions depends on process control. A controlled test lot is the most efficient way to validate performance for your use case.
Follow the supplier’s storage and handling instructions precisely. Finish-dependent products can be sensitive to improper storage conditions, so document your receiving and storage steps to maintain consistency.
To expand this practical requirement: treat receiving as part of your quality process. If your receiving area exposes the product to moisture or contamination, it can influence outcomes even when the supplier did everything correctly. Simple practices—clean staging areas, controlled humidity if required, consistent stacking methods, and careful avoidance of compression—can materially improve repeatability. Keep receiving records so that if a lot fails later, you can distinguish supplier process issues from receiving-handling impacts.
Not necessarily. If the supplier consistently provides traceable lots and your measured acceptance criteria remain stable, you may be able to reduce test frequency over time. However, any supplier change, process change, or material input change should trigger renewed testing.
A good rule of thumb is to set revalidation triggers. For example:
In those cases, revalidation protects you from spec drift and hidden internal changes.
Many buyers use finish-dependent product categories across multiple applications, but compatibility depends on the product’s stated attributes and your handling environment. Request a specification and, when feasible, validate using a test lot relevant to your industry requirements.
Compatibility isn’t just chemical or mechanical—it’s also workflow compatibility. A Fulepelata variant that works in one industry’s staging and finishing steps may fail in another industry that uses different adhesives, cleaning solutions, or heat exposure. Therefore, “cross-industry use” should be evaluated as a new use case, not a direct transplant.
Use your documented acceptance criteria and lot traceability to identify the batch. Contact the supplier promptly with photos and measurements from your test. A supplier with a clear claim process and inspection discipline can usually support corrective actions more effectively.
To improve claim outcomes, ensure you preserve evidence. For example, keep a portion of the nonconforming lot in controlled storage so it is not further altered by environment. Provide the supplier with consistent identifiers: lot ID, receiving date, storage conditions, and test results. The cleaner and more traceable your evidence, the more likely the supplier can perform a credible root cause analysis and take corrective actions.
To make future decisions about Fulepelata faster and more reliable, document the evaluation outcomes: receipt dates, storage conditions, lot ID, acceptance results, and any issues observed during handling or downstream processing. This internal record becomes your reference point for supplier comparisons and reduces uncertainty in subsequent procurement cycles.
Internal documentation matters for at least four reasons:
Consider maintaining a “Fulepelata quality dossier” that includes:
Over time, this dossier can be used to reduce requalification time. Instead of retesting everything, you can focus on changes—when a supplier maintains the same documented process and your lot traceability confirms similar internal characteristics, you can be more confident.
Risk mitigation is not just about prevention. It also includes preparedness. If a lot fails, you want to be able to quickly isolate it, document it, and decide whether to quarantine inventory, rework, or replace. Having pre-defined decision rules reduces operational chaos.
Because the earlier takeaway emphasizes verifiable controls, it helps to clarify what those controls look like at a practical level. For Fulepelata, verifiable quality controls typically include:
In a mature procurement relationship, these controls allow you to do more than accept or reject. They allow you to diagnose when quality changes and to coordinate corrective actions efficiently. For instance, if you observe a specific defect pattern in a certain month, you can use lot traceability to identify which shipments share the same internal batch profile. Then you can ask the supplier pointed questions about process settings for that production window.
It is also worth noting that verifiable controls reduce “interpretation risk.” When people rely on subjective impressions, disputes become common. When measurements and thresholds exist, disputes become less frequent and more straightforward. This is especially valuable for finish-dependent categories where human perception can vary.
A controlled test lot should not be a casual sample inspection. It should be designed to reveal failure modes relevant to how you will actually use Fulepelata. This section expands the testing strategy so you can create a test plan that predicts real-world behavior.
Begin by mapping your usage steps to likely quality sensitivities. For finish-dependent products, consider:
Then define measurable outputs. Depending on your category, measurable outputs can include:
Finally, document everything. Your documentation should include:
A strong test plan becomes a shared artifact between you and the supplier. If the supplier expects you to accept based on appearance, but you test based on measurable process outcomes, you align the relationship around objective evidence.
Quality problems are easier to resolve when communication is structured. If you’re sourcing Fulepelata, adopt communication practices that make it easy for the supplier to investigate.
When you contact the supplier—especially during test or claim—include:
Also ask targeted questions. Instead of “Why is it bad?” ask “Which process settings were used for this lot?” or “Was there any change in base material or formulation between the accepted lots and the nonconforming lot?” This helps the supplier move toward root cause faster.
When the supplier responds with incomplete information, request escalation to a quality or production technical contact. For finish-dependent categories, the most effective fixes usually require process-level understanding, not only customer service coordination.
Even after you select a supplier, you should continue monitoring Fulepelata performance. Procurement success is not just initial qualification; it’s long-term consistency.
Consider tracking a simple performance dashboard with measurable indicators:
Use this dashboard to decide when to:
Continuous improvement also means you should periodically refine your acceptance criteria. As you gain experience with how Fulepelata behaves in your process, you can define more precise thresholds and reduce evaluation ambiguity.
In procurement terms, Fulepelata should be approached as a quality-controlled product selection rather than a name-based purchase. By focusing on verifiable specifications, lot traceability, inspection standards, and controlled test validation, you can convert uncertainty into measurable confidence—leading to more consistent outcomes in both appearance and real-world performance.
When you combine documentation discipline with controlled testing and clear acceptance criteria, you reduce the risk of buying a cosmetically acceptable product that fails in your workflow. You also build an evidence-based relationship with suppliers—one where quality issues can be traced, corrected, and prevented rather than handled as recurring surprises.
Ultimately, the most effective Fulepelata sourcing strategy is straightforward: verify, test, document, and continuously monitor. If you follow that approach, you turn what could be a confusing category label into a reliably managed quality decision.
For general quality management concepts relevant to supplier process discipline, see ISO’s official materials on ISO 9001. For broader guidance on quality systems and supplier evaluation methods, consult recognized industry guidance from established standards bodies (exact applicability to Fulepelata depends on your product category and internal standards).



This guide explains how to evaluate 354679-type procurement needs with a focus on reliability, supplier capability, and compliance readiness. It provides objective background on how identifiers, vendor processes, and verification steps function in purchasing workflows. You’ll also find a comparison of options, practical requirements, and FAQs to support safer decision-making.
This guide explains how to assess the meaning and sourcing relevance of 20345690320 in procurement workflows. Objectively, identifiers and product codes often support traceability, inventory matching, and supplier verification. You’ll learn what to verify, how to compare supplier claims, which documents matter, and the practical conditions required before ordering—especially when multiple SKUs or catalog references are involved.
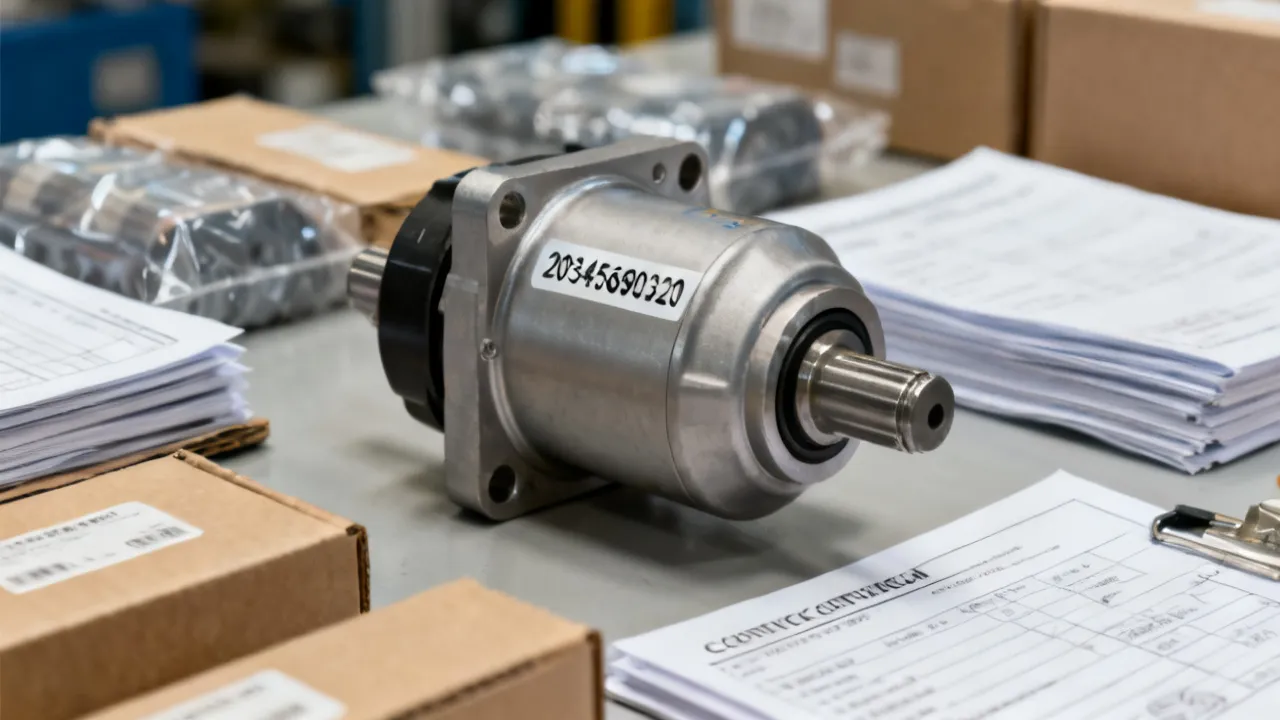
This guide explains how code “20345690320” and the identifier set in your sourcing notes can be used to structure reliable industrial procurement decisions. It provides objective background on what such identifiers typically represent, how suppliers validate compatibility, and how buyers can reduce mismatch risk by using clear requirements, controlled verification steps, and transparent acceptance criteria.
This guide explains how to evaluate item “354679” by comparing supplier offers, checking specifications, and applying practical selection criteria before purchase. Objectively, product identifiers and quote structures help buyers reduce mismatch risk, streamline procurement, and negotiate terms based on documented requirements rather than assumptions.
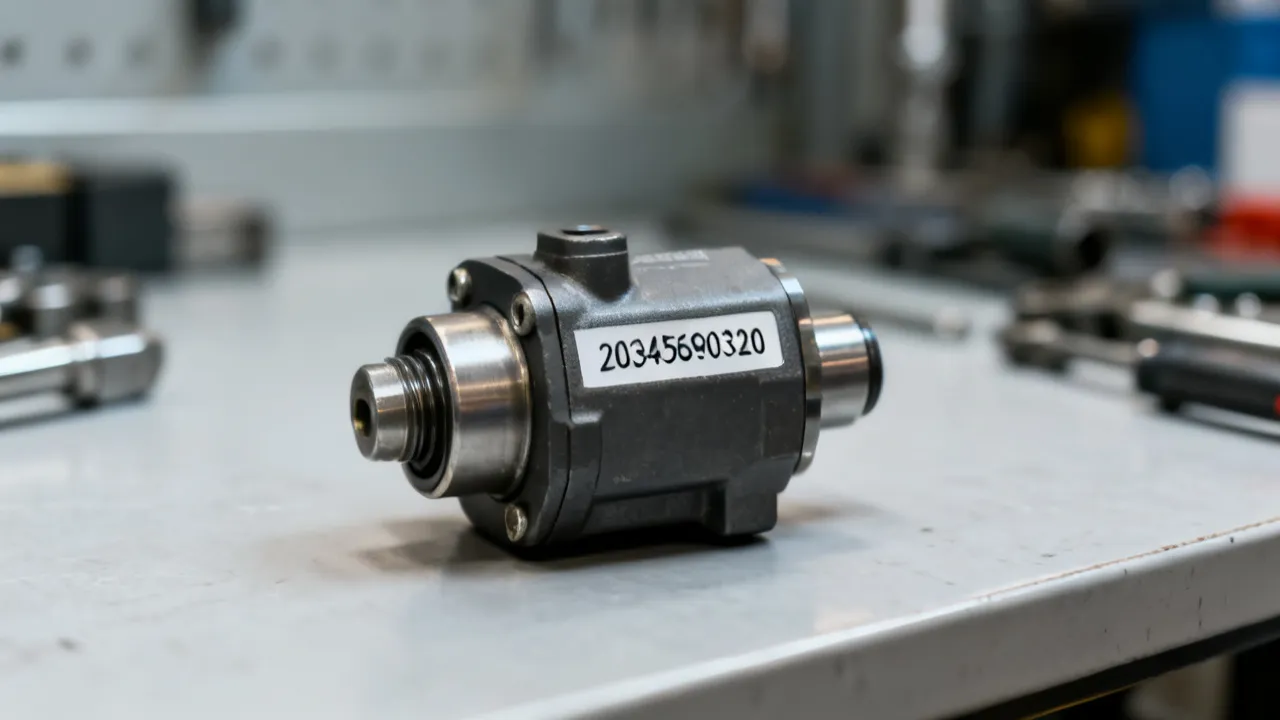
This guide explains how to interpret the identifier “20345690320” and apply rigorous supplier sourcing checks to match quality, traceability, and compatibility requirements. Objectively, the number often functions as a catalog/reference code used for procurement and verification. The article also outlines how to compare potential suppliers, validate documentation, and reduce procurement risk through structured evaluation criteria.
This guide explains how to interpret the identifier 20345690320 and how it can fit into a structured sourcing workflow, including supplier verification and documentation checks. It objectively outlines what such identifiers typically represent in procurement, inventory, and compliance processes, and provides a clear, step-by-step approach plus conditions readers should meet before placing orders.

